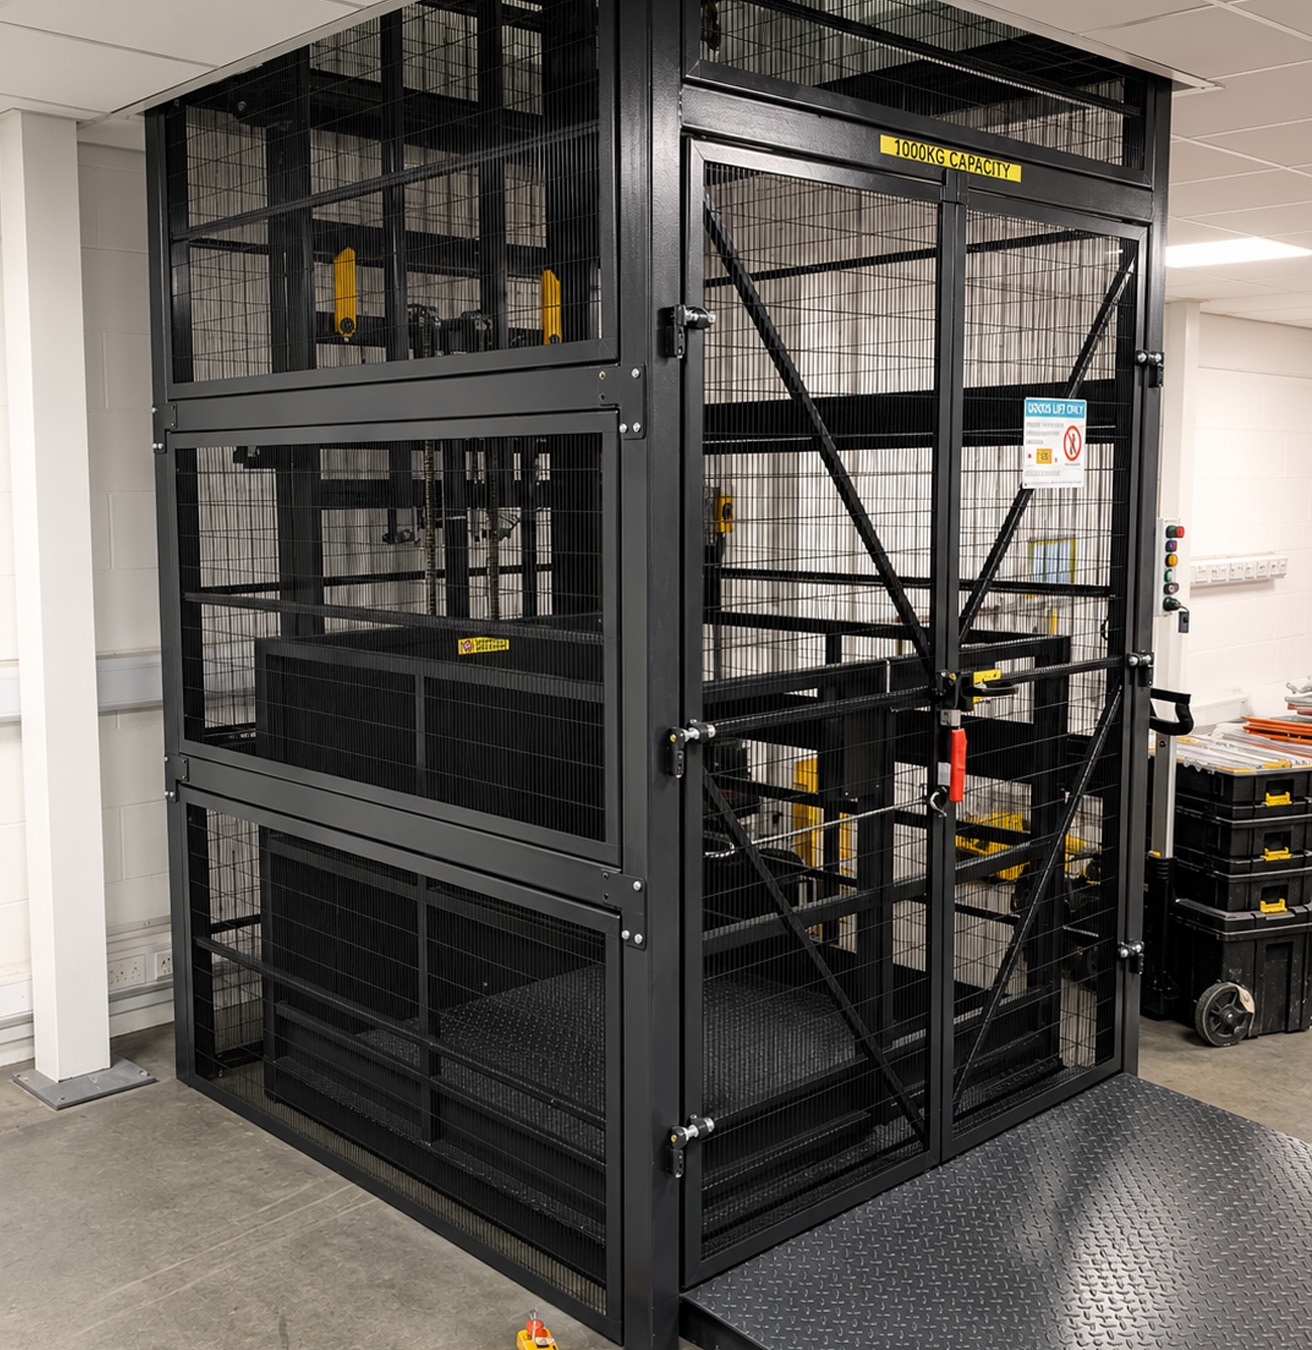
VRC / PLATFORM LIFT
The Vertical Reciprocating Conveyor (VRC) / Platform Elevator is a cost-effective, OSHA-compliant mechanical solution for moving materials - not people - between different levels of a facility. Widely used in warehousing, retail back-of-house operations, manufacturing mezzanines, and multi-tier storage facilities, the VRC provides a safe and regulated alternative to improvised solutions like forklift ramps or manual carrying.
Unlike a standard freight elevator, the VRC is classified as industrial conveying equipment - translating to significantly lower installation costs, simpler pit requirements, and faster commissioning. Platform configurations range from open to three-side enclosed or fully enclosed, accommodating everything from small parcels to full pallets and large machinery components.
Mechanical interlocks prevent the platform from moving unless all gates are properly closed at every level - zero risk of falling goods or accidental access. Simple push-button control panels on each floor require minimal operator training. Particularly popular in e-commerce fulfilment centres, printing houses, automobile parts stores, pharmaceutical warehouses, and cold chain facilities.
Request a Quote